

Products
Complete Mold Build
The whole mold, not only the plate stack — cavity and core inserts machined, fitted, assembled and spotted in the same shop.
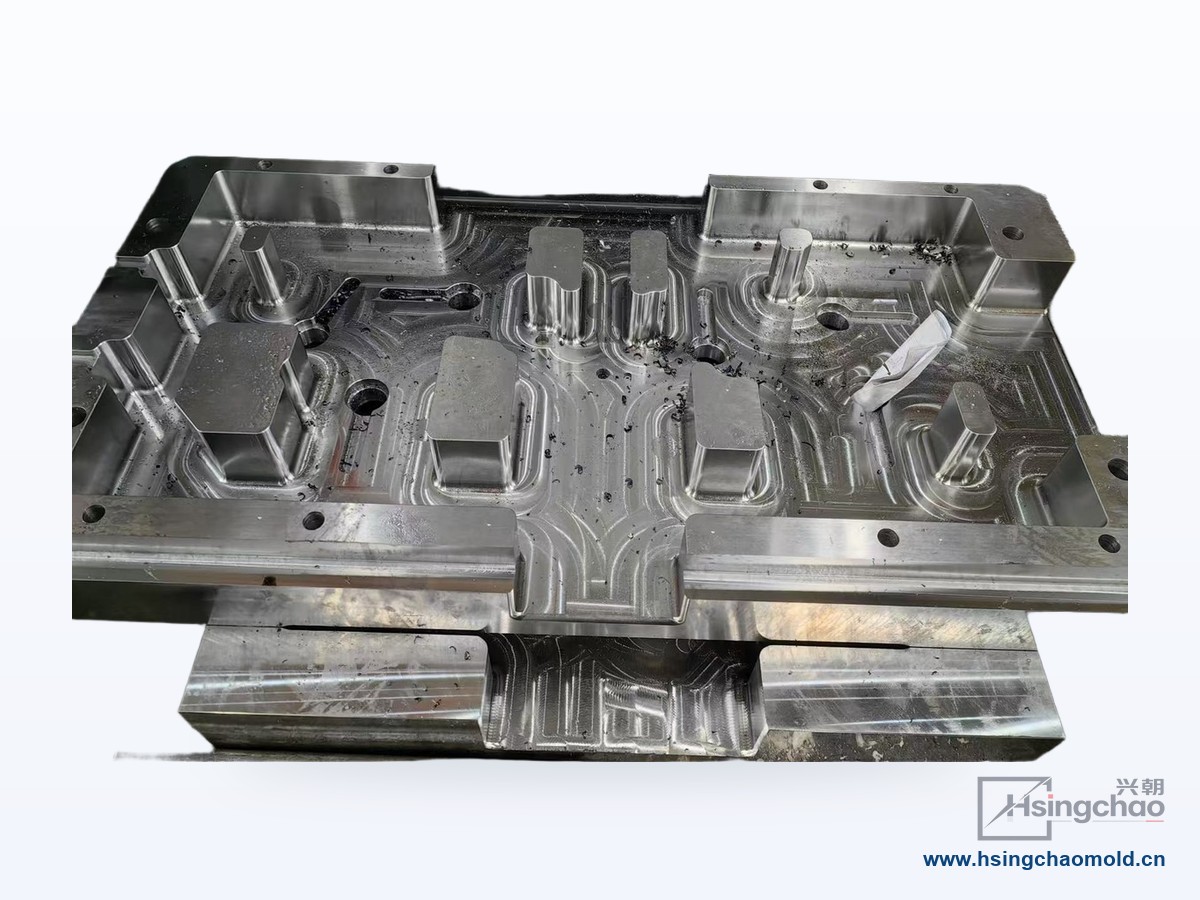
A base is only the frame. The cavity and core inserts are what actually shape your part, and we machine both. Insert blocks come off the same CNC centres as the frame, so the pocket, the shut-offs and the cooling are measured against the base they belong to rather than against a separate drawing.
Geometry a cutter cannot reach is finished by EDM and wire-cut — deep ribs, thin walls, sharp internal corners, textured faces. Steel is per your specification: 718 / 1.2738, 1.2311, or 1.2344 for die casting. Hardness and surface finish are stated on the quotation, not assumed.
Send the part model or the mold assembly as STEP or IGES, the 2D drawing with its tolerance class, the steel for base and inserts, and the machine the mold will run in — tonnage, tie-bar spacing, maximum mold height. We confirm what we will hold and where before the price goes out.
What ships: base, inserts, ejector and guide system assembled and spotted, cooling circuits fitted and blanked for transport, cavity dimensions recorded on the CMM, then film wrap and wooden case. If your own tool room prefers to finish the spotting, say so and we leave that step to you.
At a glance
7–10 day lead time for most bases · 1 set MOQ · ±0.02 mm on fitting and ground features · mold life up to 500,000 shots · CMM inspected before packing · factory direct
Related notes